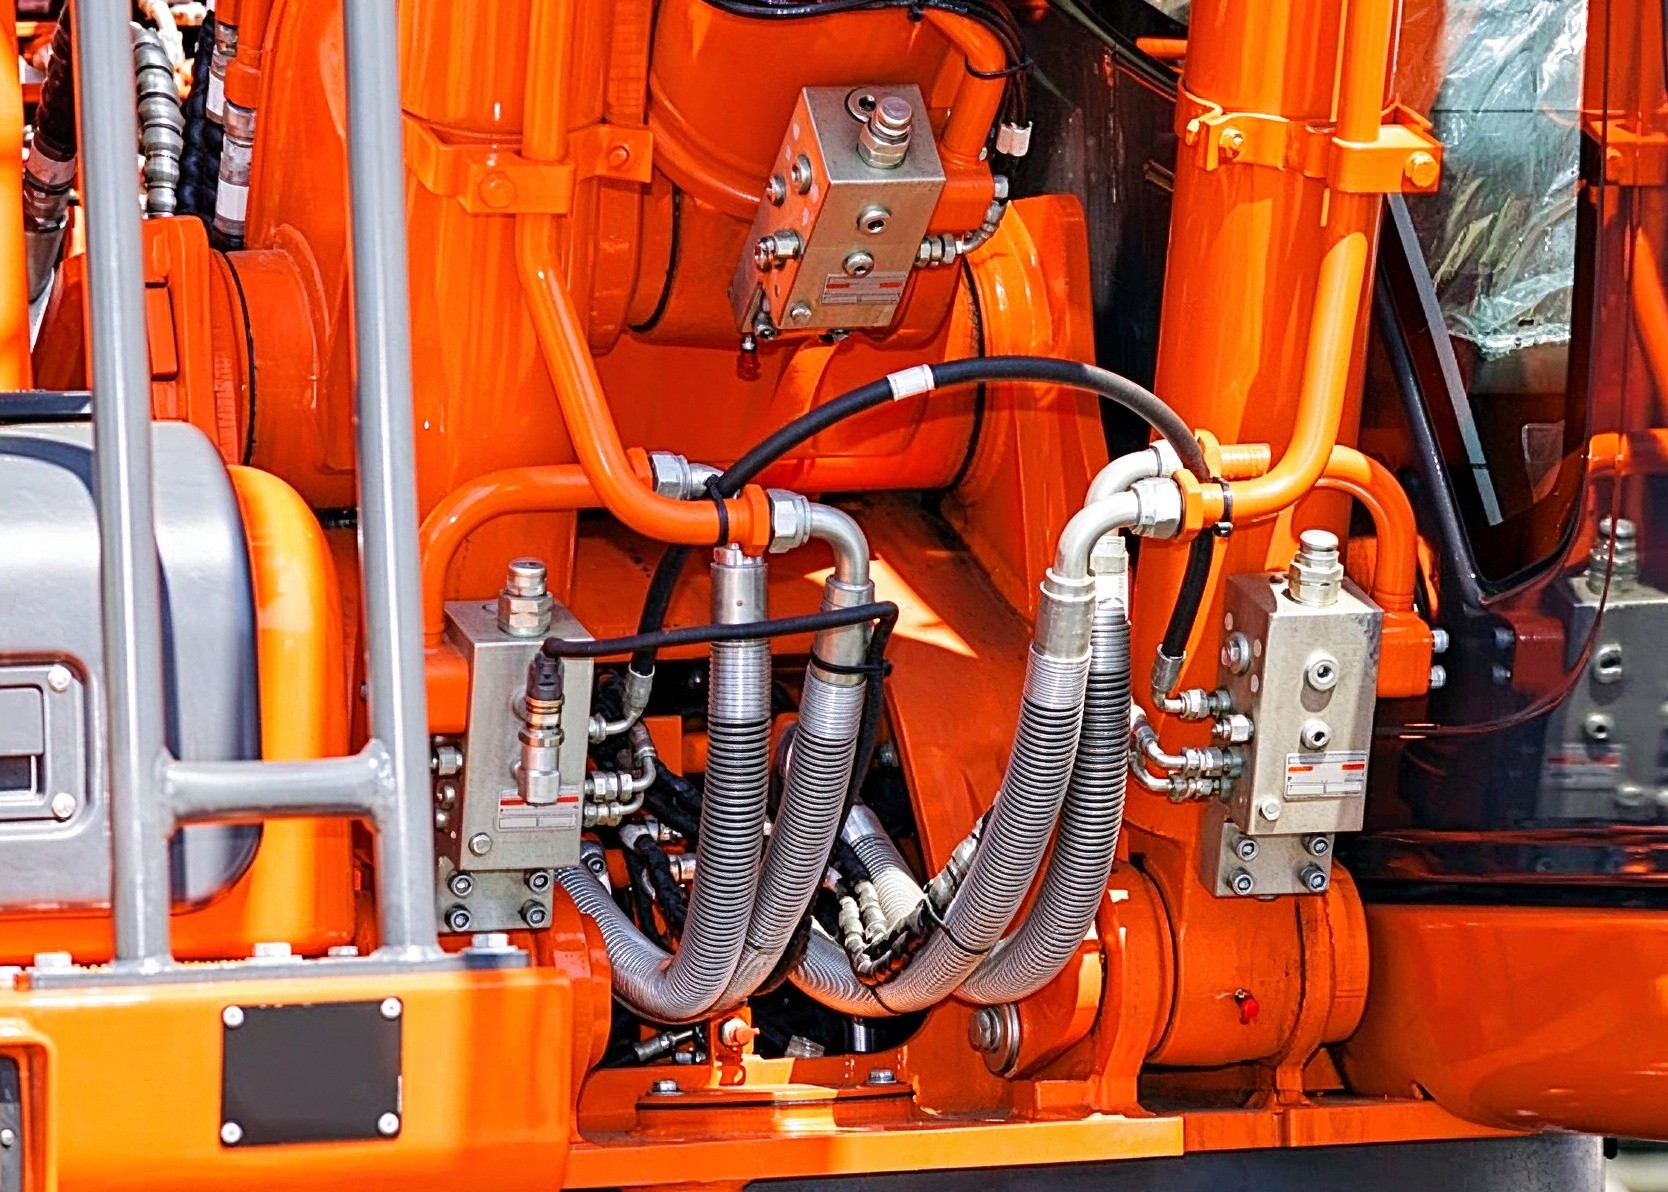
How Reinforcement Structure Governs Pressure Rating, Bend Radius and Pulse Life
Cut a high-pressure hydraulic hose crosswise, and steel wire, rather than rubber, occupies most of the cross-section area. The pressure load is borne mainly by this skeletal reinforcement. Rubber compounds bond the whole structure together and isolate hydraulic fluid from the external environment. The arrangement of the wire skeleton nearly simultaneously determines the hose’s working pressure rating, minimum bend radius and fatigue cycle life.
There are two primary wire arrangements: braided and spiral-wound. Braided construction features steel wires interlaced into a mesh, similar to plaiting. It delivers excellent flexibility and a small minimum bend radius, ideal for medium-pressure lines subject to frequent cyclic movement with machinery components. Its drawback lies in friction and contact at wire intersections; wire breakage under pulse cycling often initiates at these crossover points.
Spiral-wound construction arranges steel wires in a single-direction helix at a set angle, with adjacent layers wound in opposite directions without wire crossover. Load distribution is more uniform, generally supporting higher pressure ratings and superior pulse life. The tradeoff is substantially higher tube stiffness and a larger minimum bend radius, which may hinder installation in compact equipment spaces. These two structures are not mutually exclusive alternatives; the selection is a compromise between pressure requirements and available installation space.
More reinforcement layers do not always equal better performance. Increasing layers (2-layer, 4-layer, 6-layer) improves pressure resistance and reduces hose expansion. However, wall thickness, stiffness and minimum bend radius also rise accordingly. For hoses that swing repeatedly with booms, a 4-layer hose may not outlast a 2-layer one. Extra stiffness concentrates bending stress at the ferrule crimp zone — the very location most prone to fatigue failure.
A reliable selection workflow follows this sequence: first define the pressure rating based on the system maximum pressure, including surge peaks from valve shifting and load changes. Second, verify pulse life against cyclic frequency requirements. Finally, confirm whether the selected structure fits and bends within the actual available space on the machine. Only when all three checks pass is the structure suitable.
The interlayer rubber between reinforcement layers is not just filler. This thin rubber layer separates steel wires to prevent interlayer abrasion, permits controlled relative slippage between layers during bending, and transfers interlayer shear stress. Insufficient thickness or poor adhesion leads to delamination followed by wire fracture under pulse loads. Excessively thick interlayer rubber softens the hose, increases volumetric expansion under pressure and slows hydraulic response.
Interlayer bonding quality is validated via peel testing. Engineers distinguish cohesive failure within rubber from adhesive failure at the wire-rubber interface. Though both present as poor bonding, the two fracture modes require entirely different corrective actions. This thin interlayer rubber is rarely listed on datasheets.
Two additional variables shape performance beyond the wire skeleton: First, steel wire diameter and tensile grade. With the same number of layers, heavier-gauge wire delivers higher pressure capacity at the cost of stiffness; finer wire offers better flexibility but requires additional layers. Second, spiral pitch and winding angle. If the helix angle deviates from the neutral balance angle, the hose will elongate or contract significantly under internal pressure. Installation length allowance must account for this dimensional change. Straight end sections are required to avoid transferring axial stress directly to the crimped fittings.
This partly explains why two hoses with identical nominal size and pressure rating can behave differently when fitted to servo circuits.